01
Direct extrusion
Direct aluminum extrusion
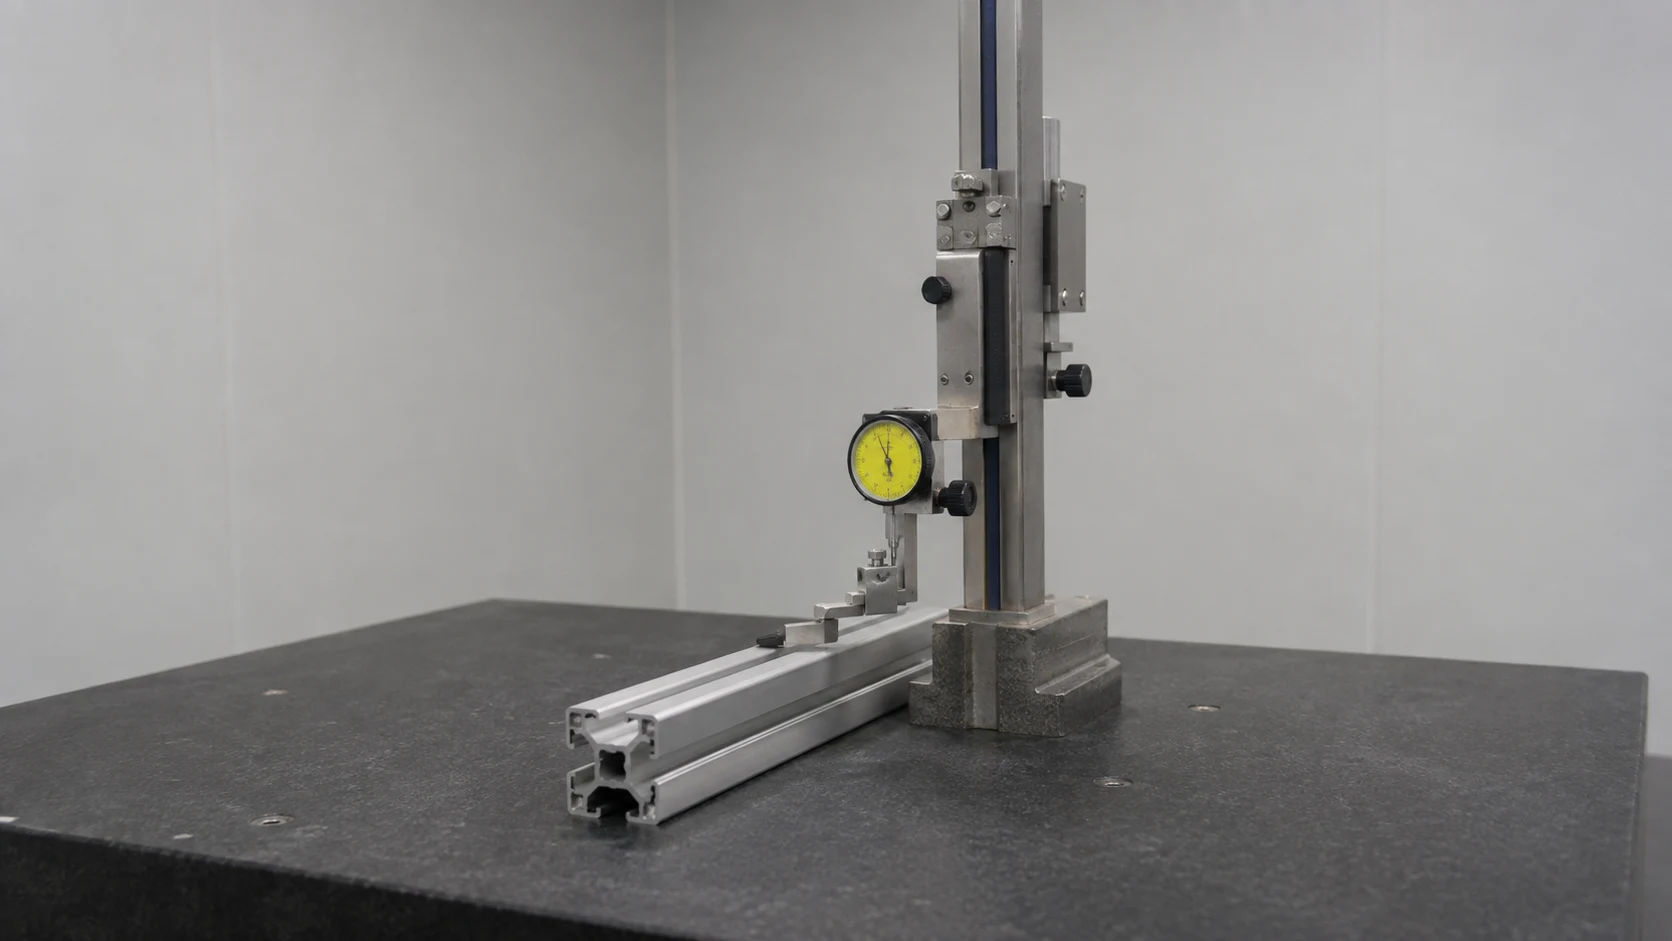
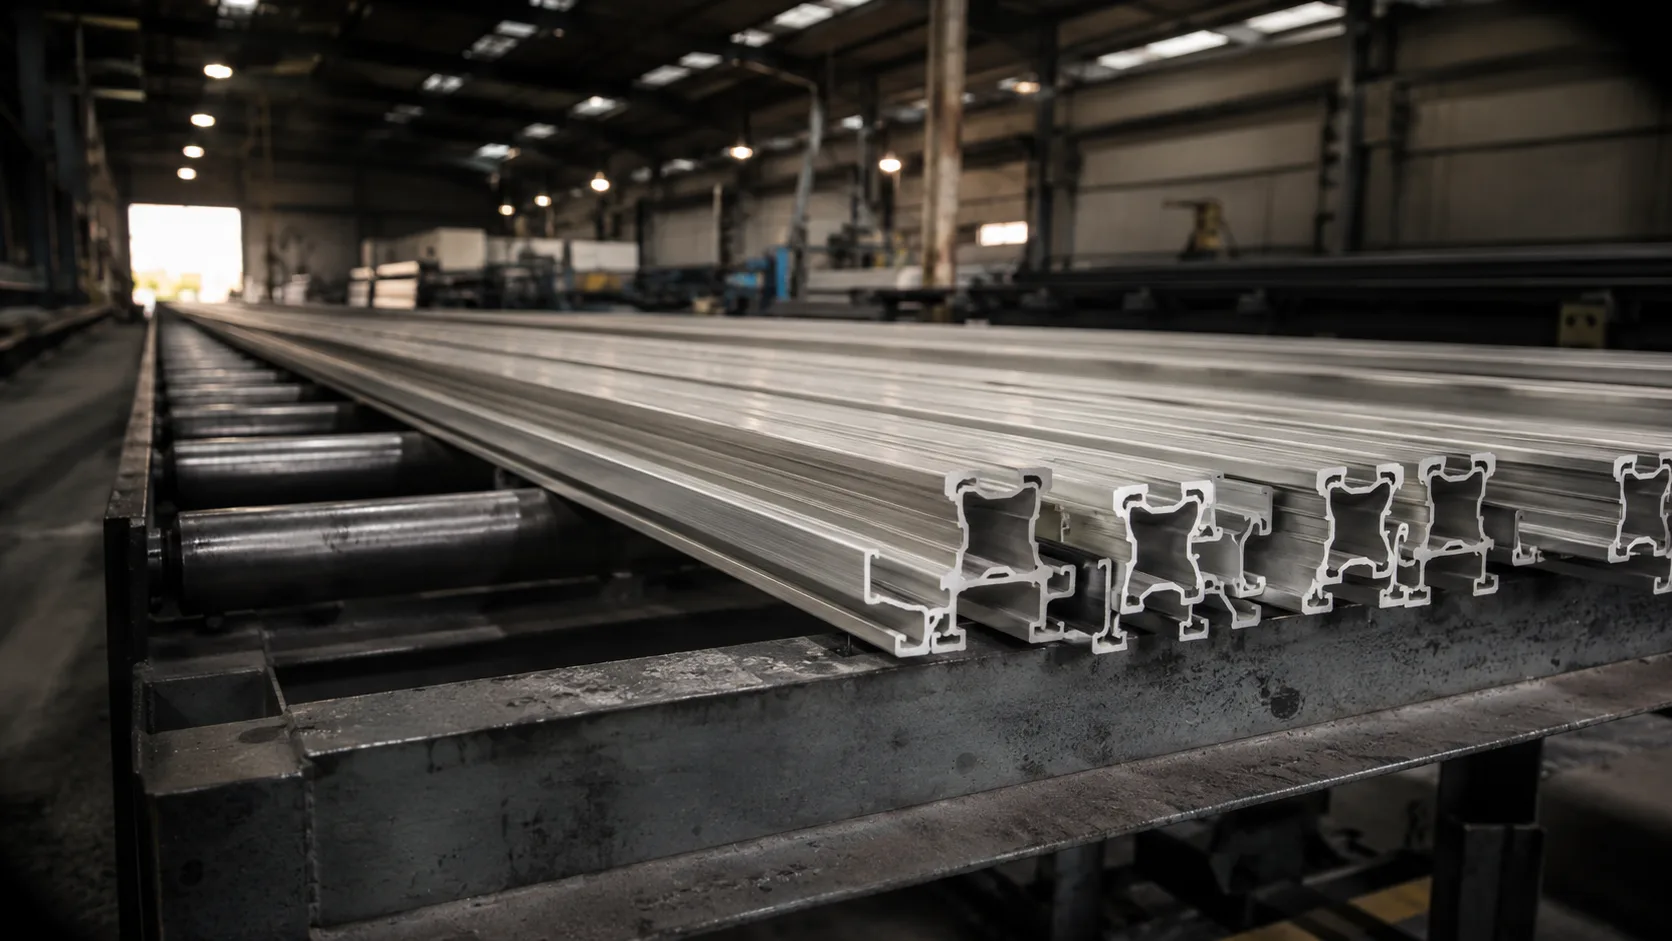
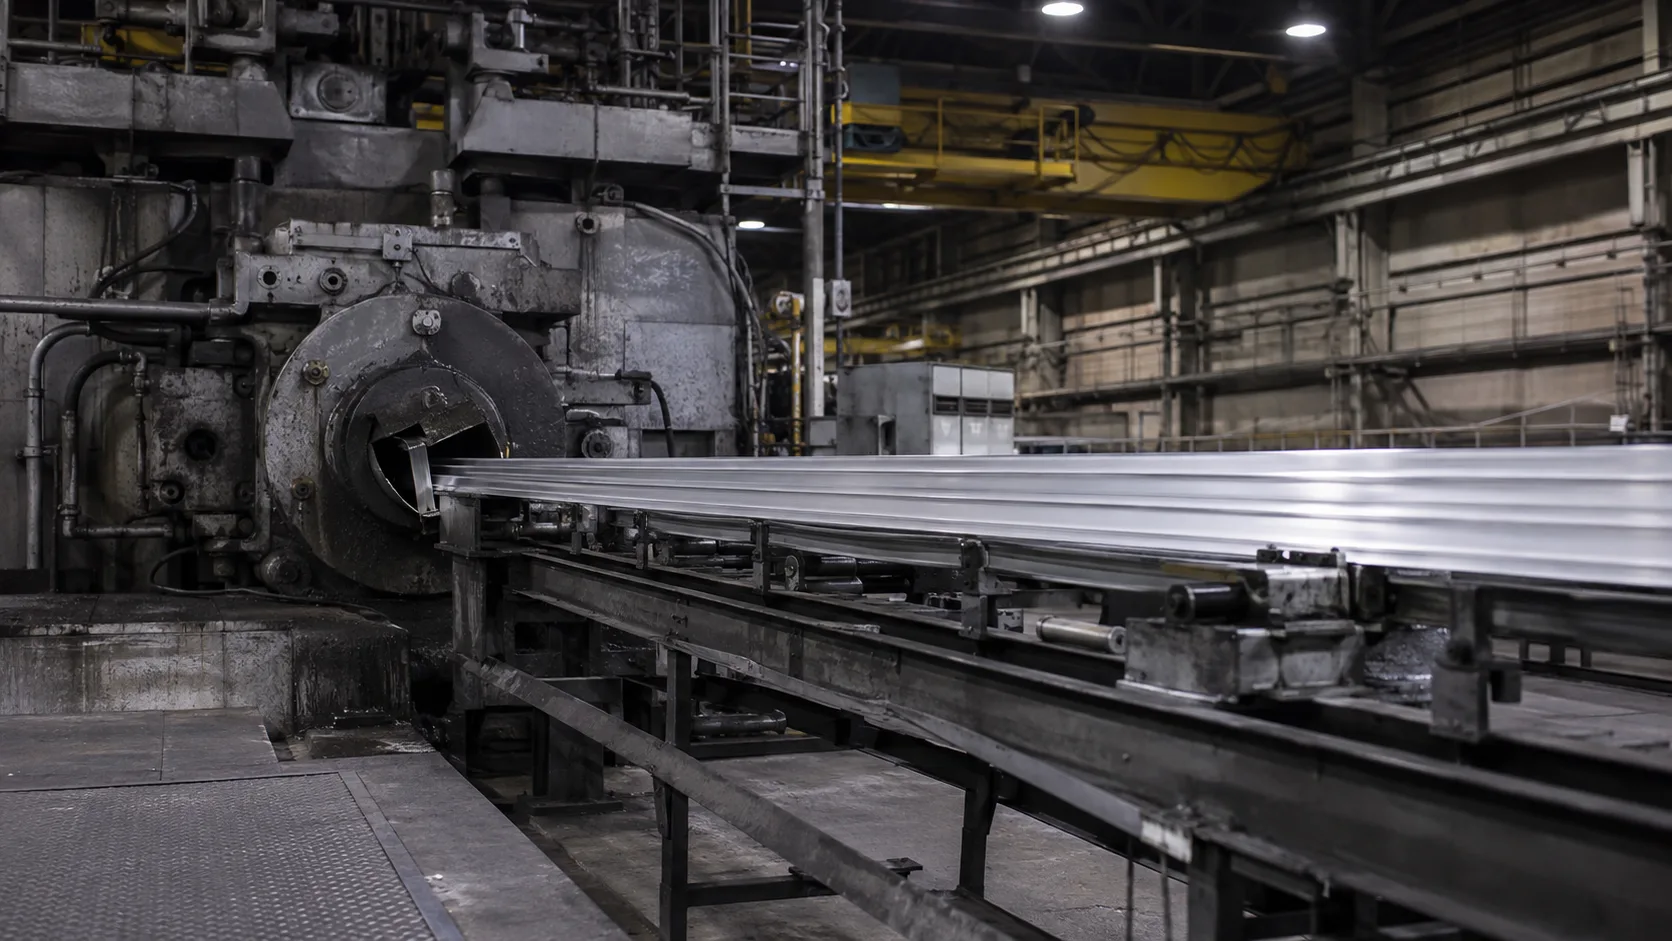
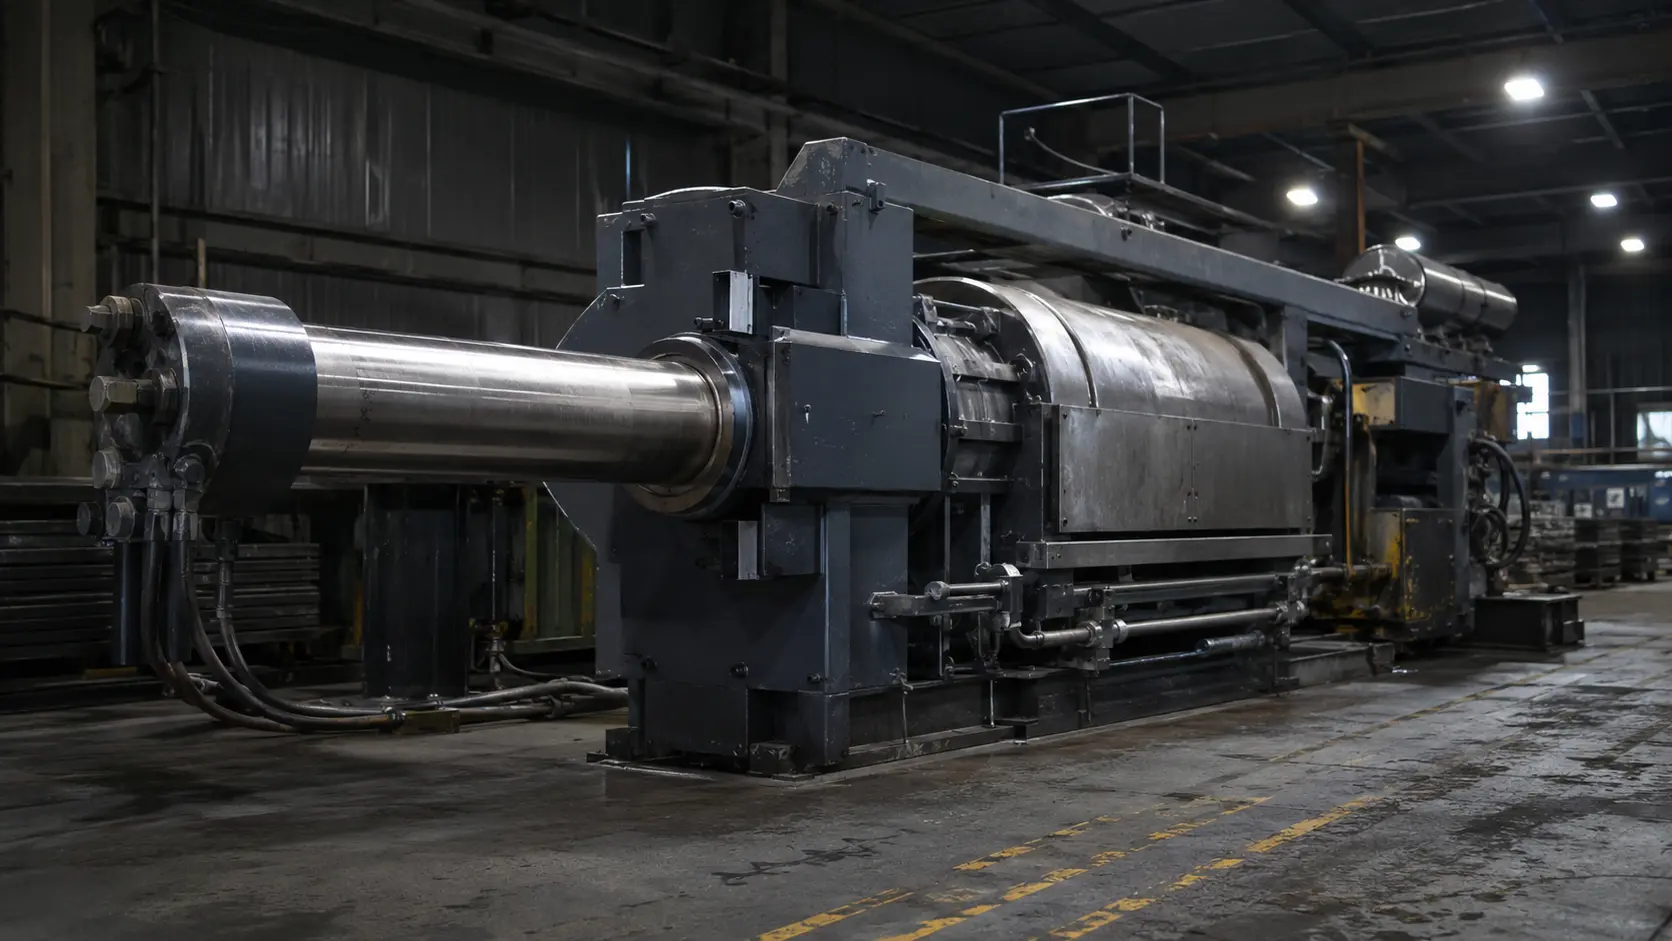
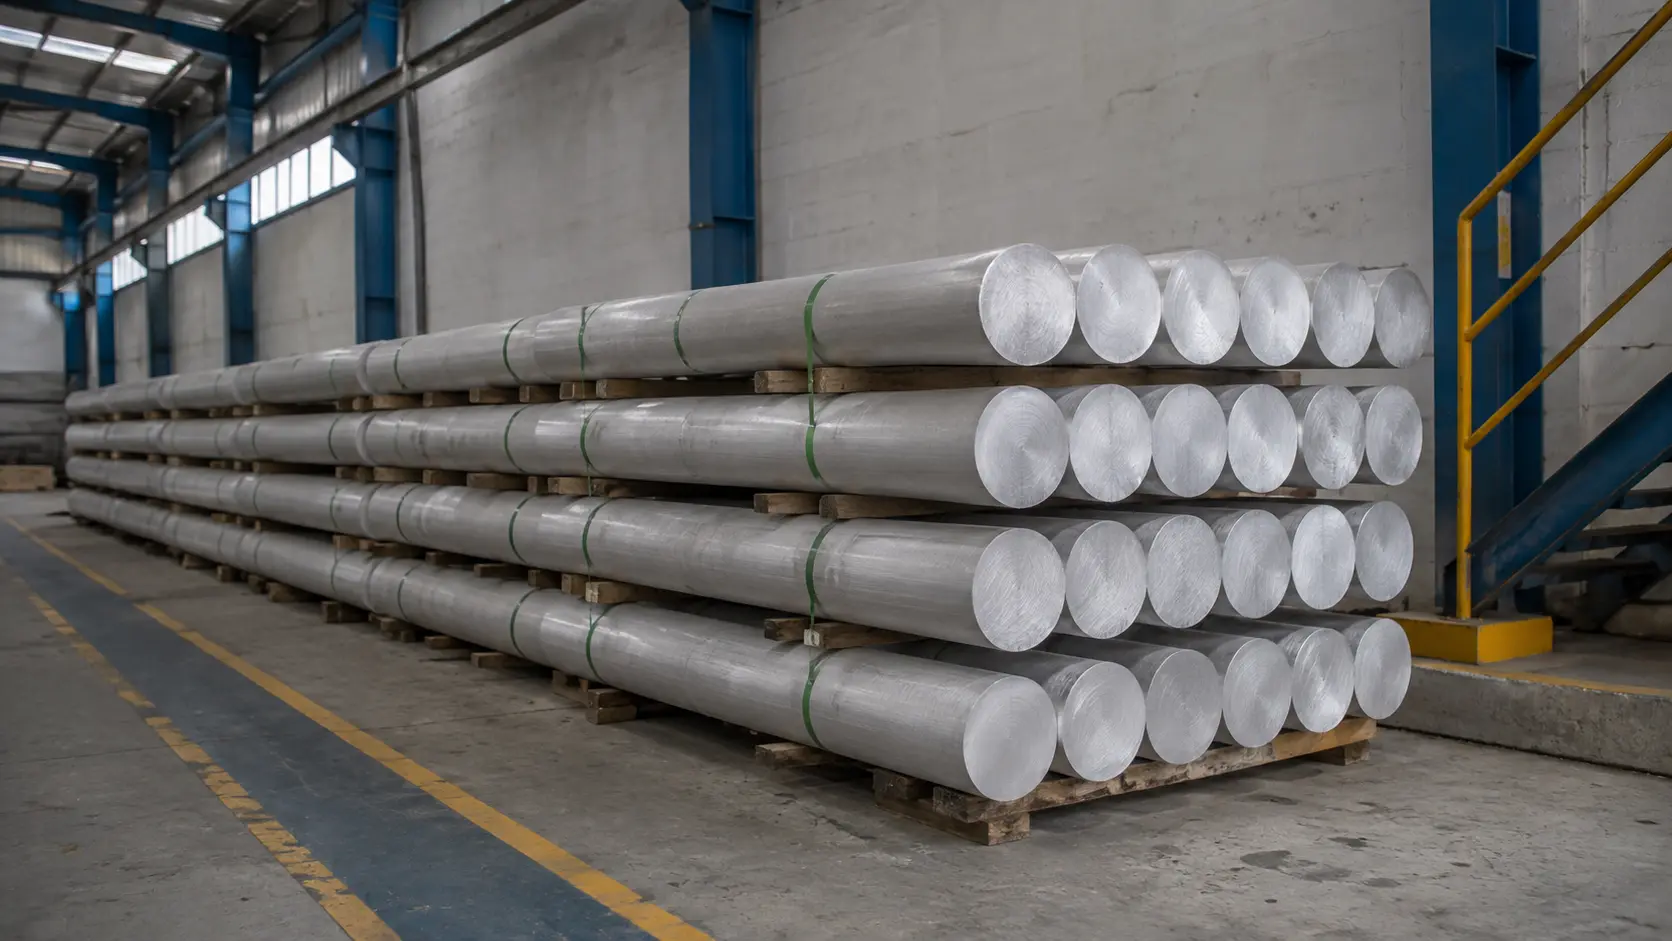
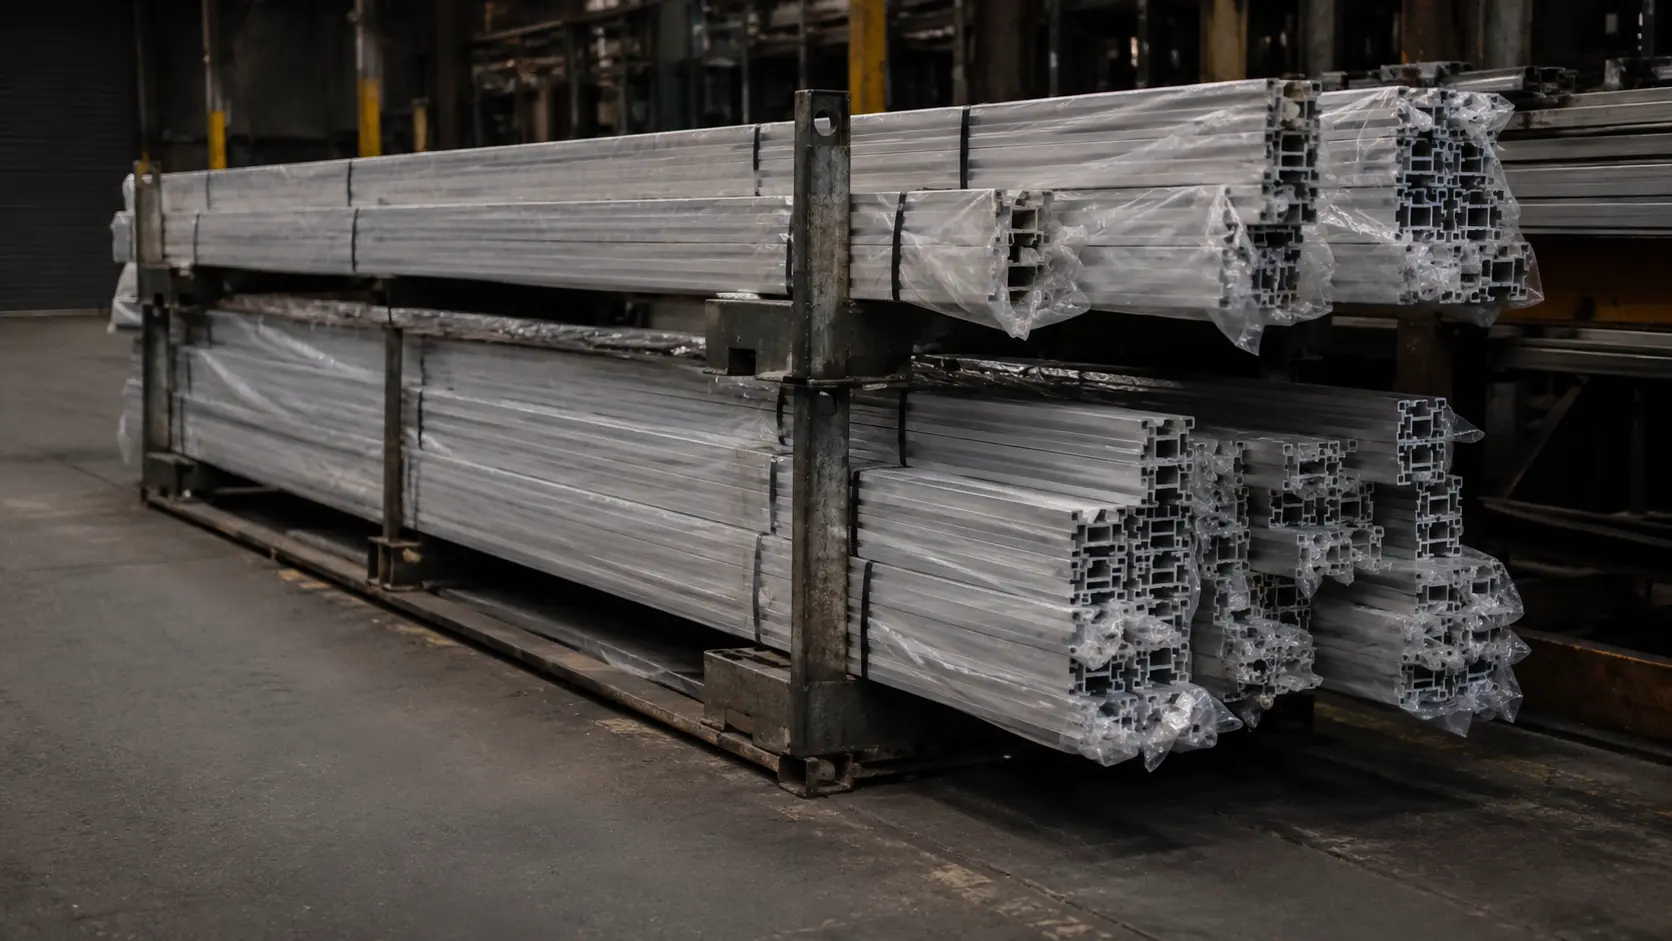
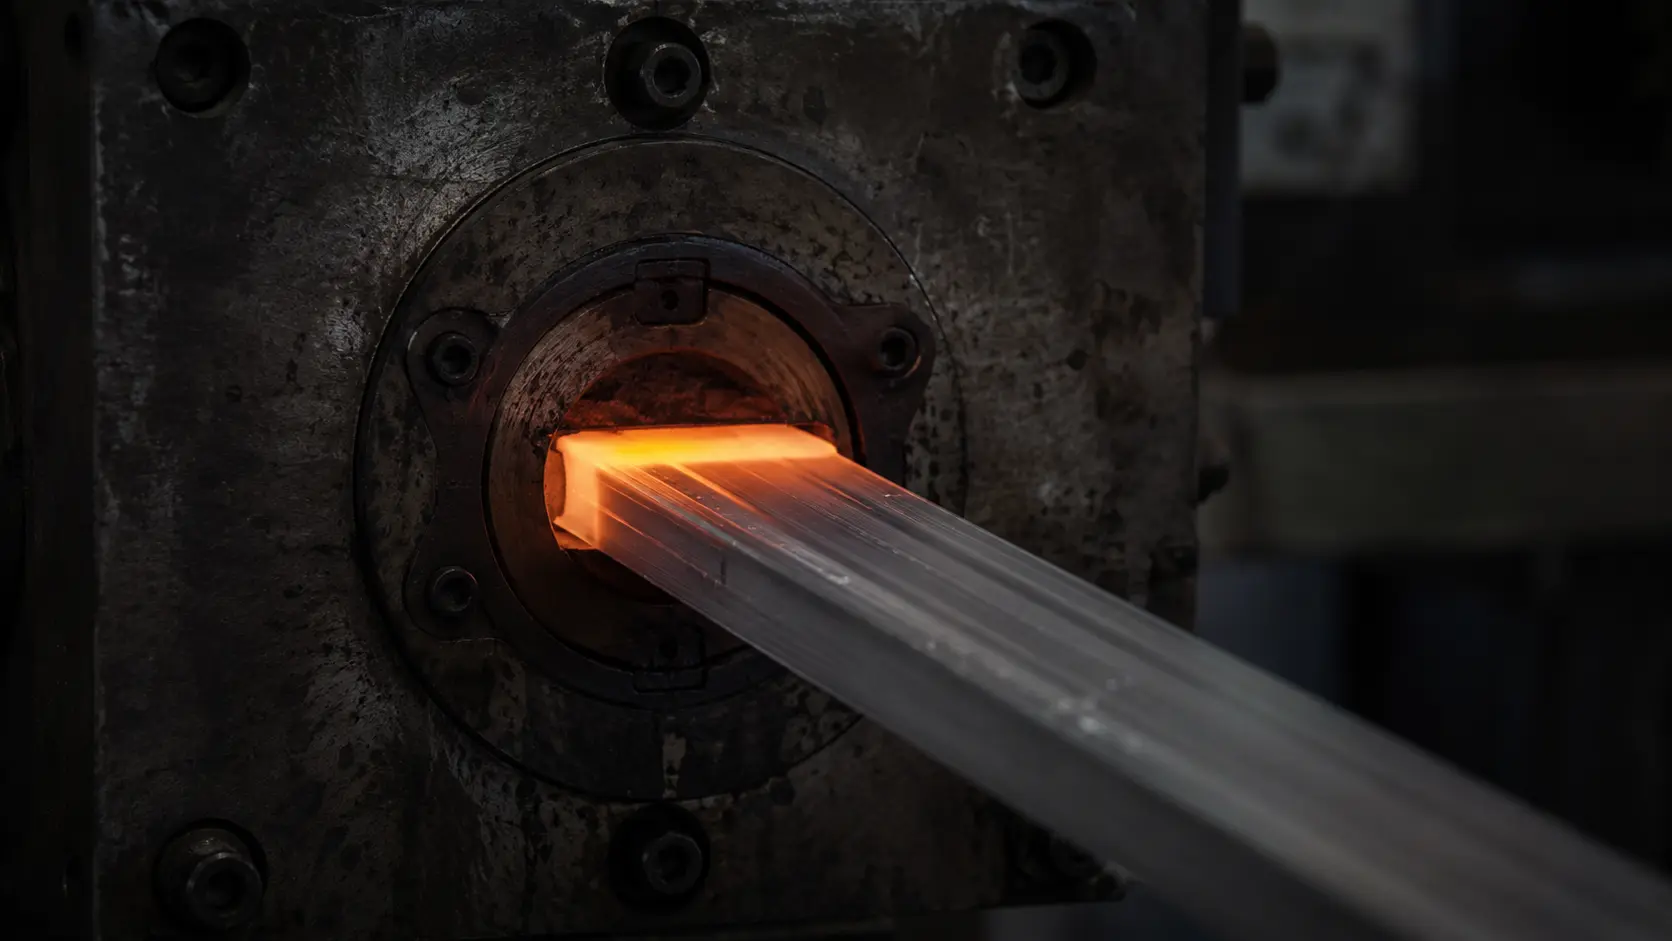
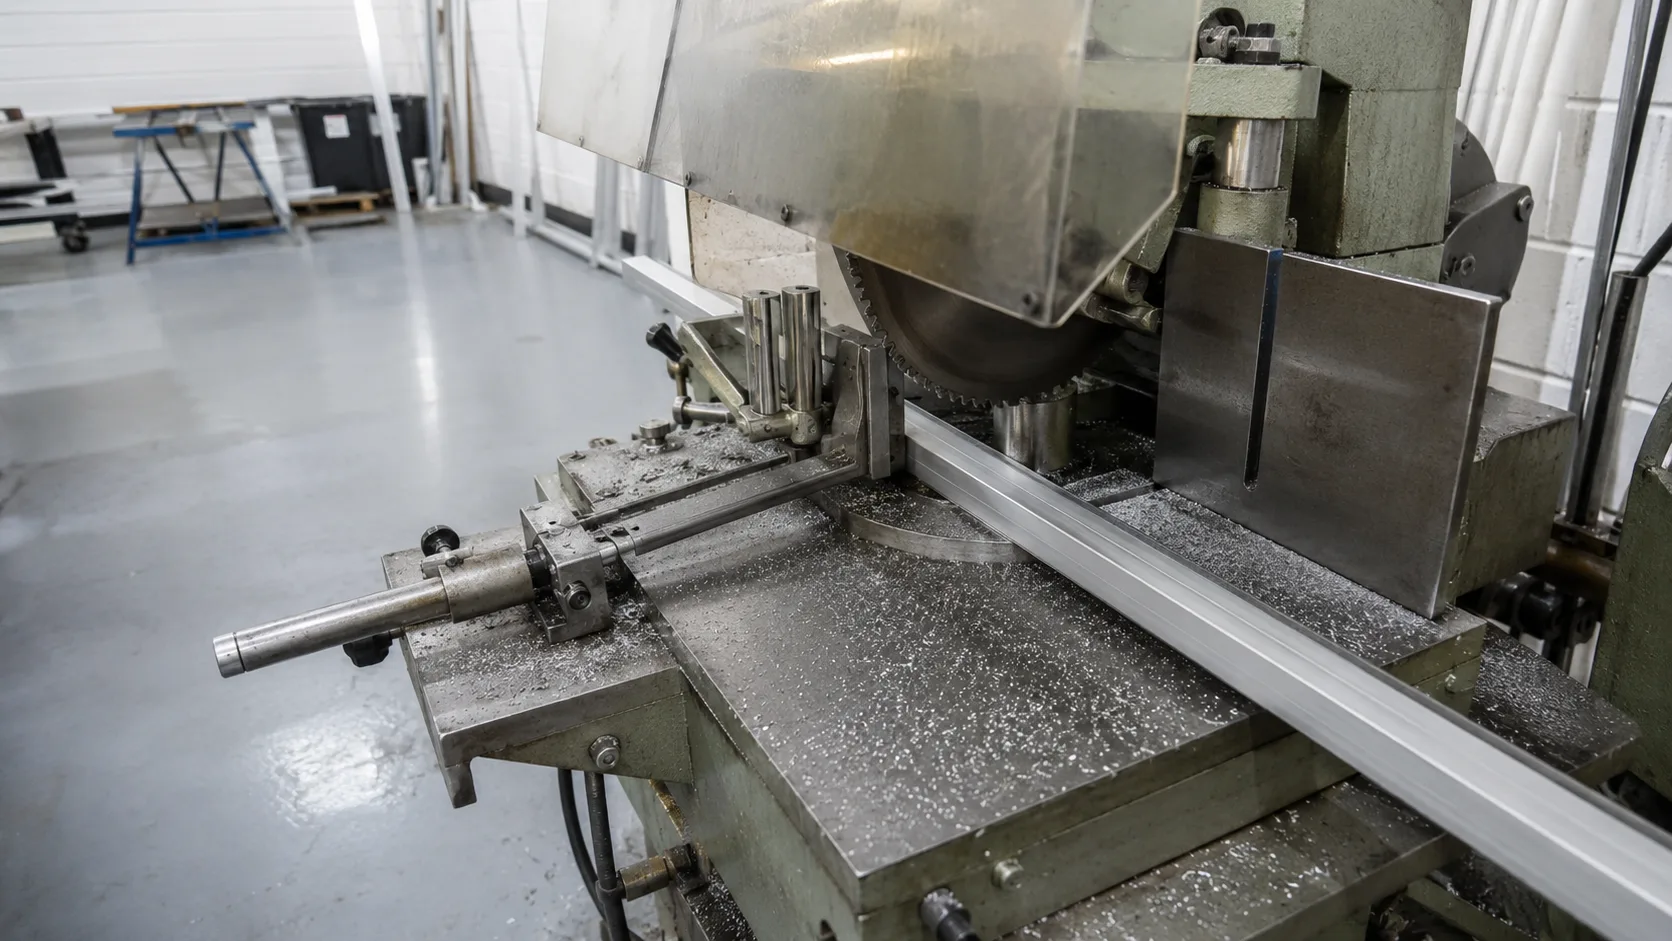
The press work. A billet heated to about 480 C is pushed through a steel die at 600 to 3,500 tonnes, then quenched, stretch straightened, and cut to mill length. Solid, semi hollow, and hollow sections up to a 250 mm circumscribing circle, walls down to 1 mm on 6063.
Press range
600 to 3500 t
Circle size
up to 250 mm